
Pharmaceutical solid dose, packing and storage
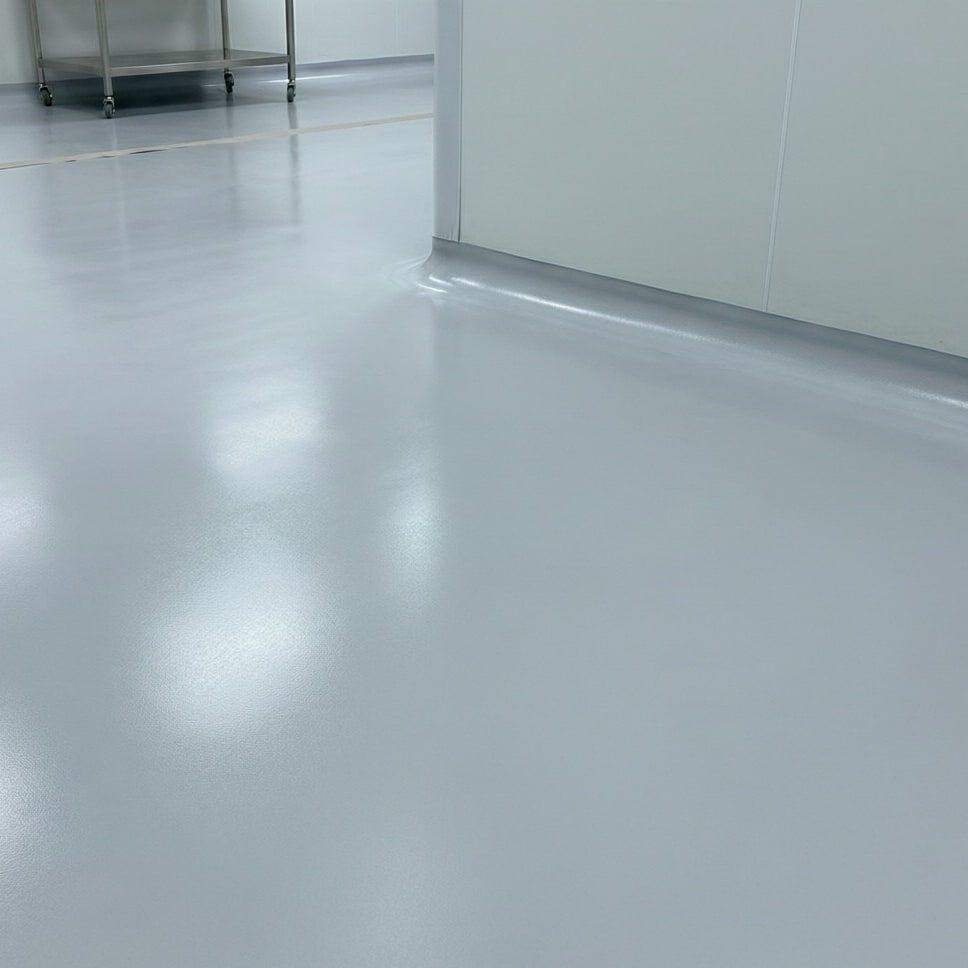
Seamless, non-shedding and coved so the wall junction is cleanable; ESD grade where powders or solvents are handled.
SKU: FW-SLF-CRN
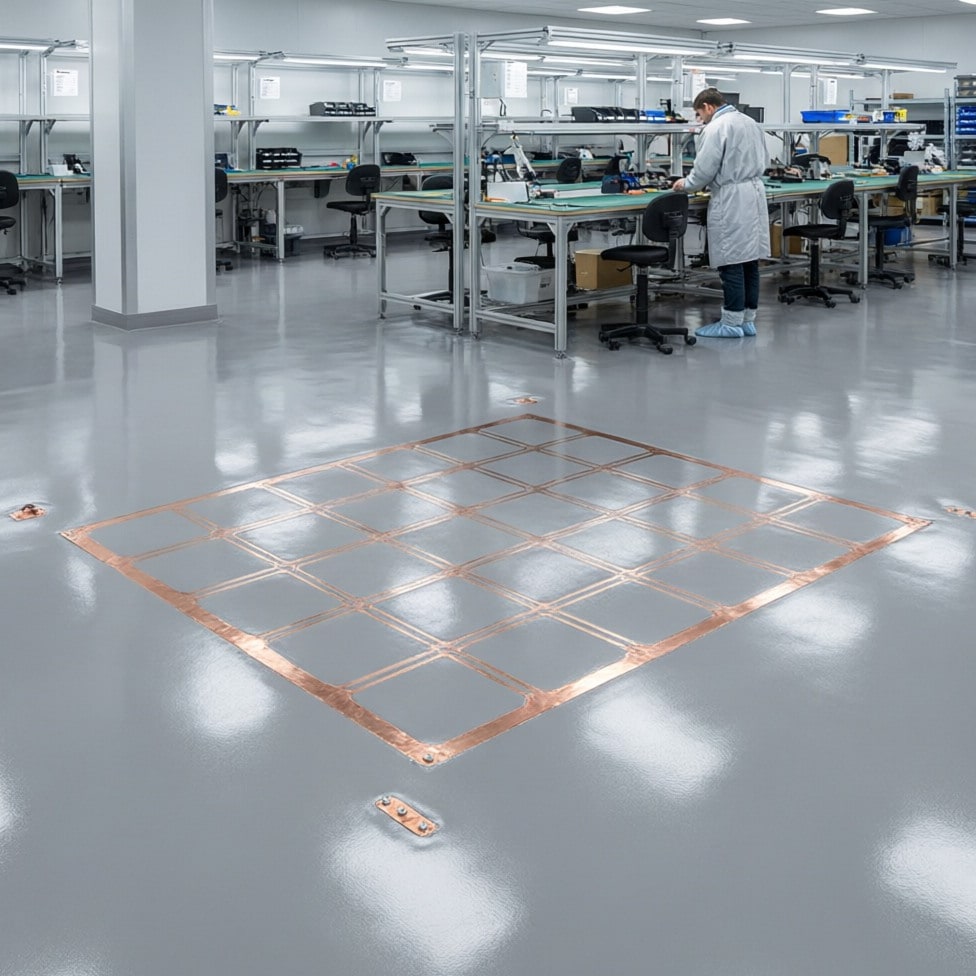
A seamless, non-shedding ESD floor supplied as a system: earthed copper grid, conductive layers, 2–3 mm antistatic self-levelling body and a coved upstand, with resistance verified on the finished floor.
Key Parameters
Standard pack: 20 kg/set (A: 15 kg + B: 5 kg). Reply within 24 hours. Custom RAL colours and OEM packaging available.
System line:Self-Leveling Epoxy > Anti-Static Self-Leveling
A seamless, non-shedding ESD floor supplied as a system — earthed copper grid, conductive layers, 2–3 mm antistatic self-levelling body and a coved upstand — with resistance verified on the finished floor, not on the paint tin.
A cleanroom floor supplied as a build-up rather than as a coating: 3 mm poured at 2.2 kg/m² per mm, low-sheen, mixed A:B = 4:1 from a 20 kg set (15 kg resin + 5 kg hardener). It holds >80 Shore D and 78 MPa compressive with 3 MPa adhesion, wears at ≤0.03 g on the Taber plate, and carries a French A+ indoor-emission classification. 30 minutes of pot life at 20 °C, walk-on at about 10 hours, full cure at 7 days.
A cleanroom floor is judged on three things and none of them is colour: it must not shed particulate of its own, it must wipe down to a dry surface, and where electronics or flammable powders are handled it must move static charge away in a controlled way. A paint-only answer fails the third, because an antistatic topcoat with nothing underneath and nowhere to discharge to is decoration, not static control — so we supply the grid, the conductive layers, the body and the earth point as one system.
The base build here is the same system as our anti-static self-leveling epoxy; what this page adds is the cleanroom detailing — the coved upstand at the wall line, the sequencing around other trades, and the record that goes with it.
In a qualified facility the floor is not signed off on appearance, so the paperwork is part of the delivery. The number that matters is measured on the completed floor, per area, under the conditions the room was actually in when it was poured — not on the paint tin and not on a test panel made in the factory. What we hand over is the build as laid, the area it covers, the ambient conditions at application, and the readings taken on the finished surface. What we do not hand over is a room classification: a floor does not make a cleanroom, the envelope, the filtration, the air changes and the pressure cascade do. Anyone offering to certify the room with the flooring is selling something other than a floor.
This is not a floor for a hot-wash bay, a steam-cleaned area or a cold room — those need a binder chemistry we do not manufacture, and we will say so rather than sell you a floor with an expiry date. A production area that needs static control for electronics but has no classification paperwork is better served by the base anti-static build. Send the room list, the cleaning agents with their dilutions, and the resistance your spec writer has called for: the target comes from your qualification document, not from our data sheet.
A cleanroom floor is judged on three things and none of them is colour. It must not shed particulate of its own, it must be possible to wipe right down to a dry surface, and — where electronics or flammable powders are handled — it must move static charge away from people and equipment in a controlled way. A paint-only answer fails the third one, because an antistatic topcoat with nothing underneath and nowhere to discharge to is decoration, not static control.
So we specify this as a build-up: substrate thresholds confirmed first, then a copper tape grid tied to a documented earth point, a conductive primer and intermediate layer over it, the antistatic self-levelling body at 2–3 mm, and a coved upstand of the same material at the wall base. Resistance is then measured on the completed floor and recorded, because that is the only number that means anything to your validation file.
What we do not claim. A floor does not make a room ISO Class — classification is a property of the whole room (envelope, filtration, air changes, pressure cascade and behaviour) and is verified on site. And the wet, hot-washed rooms in a food plant — cook-line floors, CIP areas, wash bays — need a polyurethane cement mortar system; we do not manufacture it, and we will say so rather than let you discover it after handover.
| Substrate | Thresholds confirmed firstCompressive ≥ 25 MPa, moisture < 4 %, pH < 9, 2 m straightedge gap ≤ 2 mm |
|---|---|
| Prep | Grind + vacuumRemove laitance, old sealers and any adhesive residue; dust extraction throughout |
| Earth | Copper tape grid + earth pointGrid laid and tied to a documented earth; continuity checked and recorded before anything covers it |
| Conductive layer | Primer + intermediateConductive epoxy primer worked into the grid, then the conductive intermediate coat |
| Body | 2–3 mm antistatic self-levelling≈ 2.2 kg/m² per mm, squeegee-poured and spiked; coved upstand formed at the wall base |
| Finish | ESD wear coatLow-sheen, cleanable; then resistance is measured, recorded and handed over |
Custom RAL matching available — we ship a physical sample card before production.
| Brand | Friway |
|---|---|
| SKU | FW-SLF-CRN |
| Category | Self-Leveling Epoxy > Anti-Static Self-Leveling |
| Finish | Low-sheen / satin |
| Coverage | 2.2 kg/m²/mm |
| Thickness | 3 mm |
| Mix Ratio | A:B = 4:1 |
| Pot Life | 30 min |
| Walk-on Time | 10 h |
| Full Cure | 168 h |
| Hardness | >80 Shore D |
| Adhesion | 3 MPa |
| Compressive Strength | 78 MPa |
| Abrasion Resistance | ≤0.03 g (Taber CS-17, 1000 cycles) |
| Package | 20 kg/set (A: 15 kg + B: 5 kg) |
| Warranty | 3 years |
| Surface resistance | 1.0×10⁶–1.0×10⁹ Ω (dissipative grade)Design target for the finished system; conductive grade specified at < 1.0×10⁶ Ω |
|---|---|
| Where it is measured | On the completed floorNot on the paint alone — we record the build, the area and the ambient conditions |
| Substrate strength | ≥ 25 MPa compressiveAn ESD floor over a weak slab is a demolition job waiting to happen |
| Substrate moisture | < 4 % CM, pH < 9Ground-floor slabs without a working DPM are tested before we quote |
| Flatness | 2 m straightedge ≤ 2 mmA 2 mm self-levelling body follows the slab; it does not correct it |
| Ambient | 10–25 °C, RH ≤ 75 %Slab 3 °C above dew point; run the HVAC during application, not after |
| Walk-on | 8–12 h at 20 °CGowning traffic only after the wear coat has set |
| Return to service | 72 h light / 7 d fullWet cleaning and equipment wheels after full cure |
| Compressive strength | 78–80 MPaSelf-levelling build at 7 d / 20 °C |
|---|---|
| Bond | ≥ 3.0 MPaConcrete failure on a profiled slab |
| Hardness | > 80 Shore DTrolleys and racking on soft castors; not a forklift floor |
| Abrasion | ≤ 0.03 gTaber CS-17, 1000 cycles |
| Cleaning agents | Good resistance to quats, 1 % hypochlorite and 70 % IPAStanding bleach will dull and discolour — dilute, time it, then rinse |
| Particulate | Non-shedding seamless surfaceSupports classification; it is not itself a classification |
| Not suitable for | Steam-cleaned or hot-wash bays, cold roomsThose need PU cement mortar — we do not manufacture it |
Figures are typical values measured in our laboratory. Substrate, climate and workmanship affect the result — we confirm the final specification in writing before your order.
We release documents as editable originals on request (batch-specific data is not in a generic PDF). One click sends your request with this product attached.
Two-component sets palletised for export, shipped fromDongguan, Guangdong, China by Dongguan Friway Hydraulic Control Technology Co., Ltd..
| Set composition | 20 kg/set (A: 15 kg + B: 5 kg) |
|---|---|
| Net weight / set | 20 kg |
| Pallet configuration | 24 sets (480 kg net) per 1200 × 1000 mm pallet, stretch-wrapped with corner boards |
| 20 ft container | ≈ 480 sets |
| 40 ft HQ | ≈ 960 sets |
| Shelf life | 12 months from fill date |
| Storage | Dry, ventilated store, 5–30 °C; protect from frost and direct sunlight. Keep sealed — Part B absorbs moisture from air. |
Counted from confirmed deposit and approved colour. FOBShenzhen or Guangzhou; CIF and DDP quoted on request.
| Order quantity | Lead time | Notes |
|---|---|---|
| Sample (≤ 2 sets) | 2–4 days | courier freight collect via DHL / UPS / FedEx, shipping at your cost; 5–7 days door to door |
| 1–49 sets | 5–7 days | Stock colours first; standard export packing included |
| 50–199 sets | 10–12 days | Includes batch mixing and in-house QC record per batch |
| 200–999 sets | 15–20 days | Production slot reserved after 30% deposit |
| FCL / 1000+ sets | 22–28 days | Confirmed against the shipping schedule; FOB Shenzhen or Guangzhou |
RAL / Pantone reference or a physical sample; we send a wet film for approval before batch production.
Your logo and language on the pails and carton; artwork in AI/PDF. Blank labelling available below this MOQ.
Pail size, carton printing, palletising and shipping marks per your export requirement.
Formulation adjustment (gloss, cure speed, aggregate, conductivity range) with TDS and CoA issued under your brand.
Company-level documents we can issue for this system. We supply certificate copies and batch test reports on request rather than publishing them as images.
Agree the electrical and validation requirement firstWeek −3
Which grade, which rooms, where the earth point is, and who signs off the resistance record. This decides the build-up before any colour does.
Confirm the slabDay −2
Compressive, moisture and pH readings plus a 2 m straightedge check. Fix the slab now — a resin overlay will not rescue it later.
Grind and extractDay 1, 4–6 h per 200 m²
Diamond-grind to open the profile, remove every trace of sealer and old adhesive, and keep dust captured — cleanroom work is dusty until it is not.
Lay the copper grid and tie it to earthDay 1–2
Tape laid in the grid pattern, tied to the documented earth point, then continuity-checked and photographed before anything covers it. Once it is under resin you cannot inspect it.
Conductive primer and intermediateDay 2, then 12–16 h
Worked into the grid so the charge has a continuous path from the surface down to earth. Gaps here are the usual cause of a failed reading.
Form the cove, then pour the bodyDay 3, 2–4 h per bay
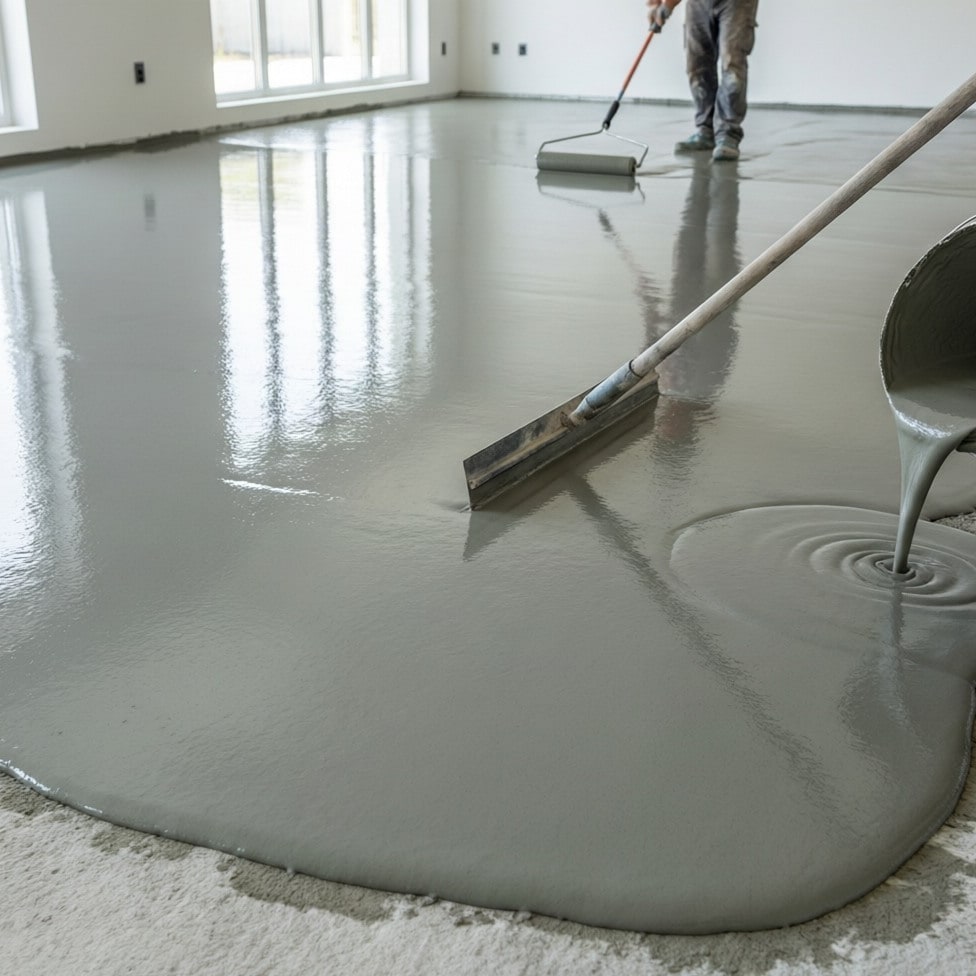
Coved upstand at the wall base first, then 2–3 mm antistatic self-levelling gauge-spread and spiked. One bay per shift, no cold joint across a doorway.
Wear coat, measure, hand overDay 4, then 7 d
Low-sheen ESD wear coat, then surface resistance measured across the floor and recorded with area and ambient conditions. That record is what goes in the validation file.
Need the full method statement for your site? Request it with the form below — we review your slab data before your crew starts.
Seamless, non-shedding and coved so the wall junction is cleanable; ESD grade where powders or solvents are handled.
Static-dissipative or conductive grade to keep charge away from components, with the earthed grid as part of the build.
Cleanable surface plus documented resistance readings for the technical file.
Sample preparation, stores and instrument rooms — spills wipe up, and the cove removes the dirty corner.
Where the floor sees footfall and packaging, not hot wash. Wet and steam-cleaned bays are a different system.
No, and a supplier who says so is overselling. Classification is a property of the whole room — envelope, filtration, air changes, pressure cascade and operator behaviour — measured after commissioning. What the floor contributes is a seamless, non-shedding, cleanable surface with no joints to harbour particulate, which is exactly what a cleanroom specification asks of a floor.
It depends what you are protecting. Static-dissipative (surface resistance 1.0×10⁶–1.0×10⁹ Ω as a design target) is the usual choice for electronics assembly and general GMP areas. Conductive (< 1.0×10⁶ Ω) is specified where component handling or flammable vapours and powders demand faster, lower-resistance discharge. Tell us the process and we will specify the grade rather than guess.
Yes — that is the part most quotations quietly leave out. Without an earthed copper grid tied to a documented earth point, a dissipative surface simply holds the charge. We lay the grid, continuity-test it, photograph it before covering, and measure the finished floor.
Over fully bonded, non-foam-backed vinyl that has been abraded and primed, usually yes. Foam-backed or loose-laid sheet must come out completely — the conductive path and the bond both have to reach the slab, not a layer of adhesive.
Quaternary ammonium disinfectants, 70 % isopropyl alcohol and 1 % sodium hypochlorite are all fine at correct dilution with a clean-water rinse after contact time. What damages floors is undiluted or standing bleach and abrasive pads, not the chemistry itself.
Walk-on in 8–12 hours at 20 °C, light gowning traffic and trolleys from 72 hours, full wet cleaning and equipment at 7 days. We phase the work bay by bay so a live facility keeps running.
Not with epoxy, honestly. Hot-wash, steam-cleaned and sub-zero floors are thermal-shock duty and need a polyurethane cement mortar system, which we do not manufacture. Tell us the cleaning regime and the temperature and we will say which rooms our system fits and which it does not.
Yes — the grid, the earth point detail and the conductive layers ship as part of the system, with the layout drawing. Supplying only the topcoat and hoping the contractor works the rest out is how ESD floors fail acceptance.
Your project has conditions we cannot see from here? Send the slab report and drawings — our engineers answer with a written specification.
Dongguan Friway Hydraulic Control Technology Co., Ltd.
Every batch of Cleanroom & GMP Antistatic Epoxy Floor System is produced in our own facility by a team that integrates R&D, production, sales and technical service. Advanced equipment, batch-level lab testing and a complete quality system mean consistent quality — from the first sample to the last pallet.
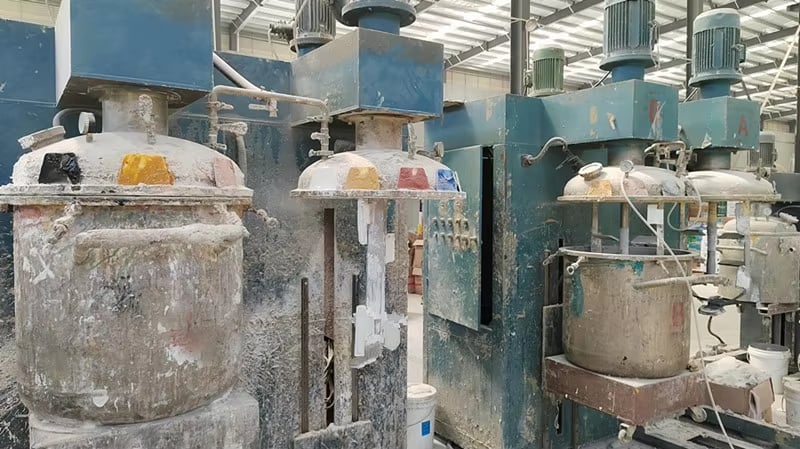 Mixing Lines
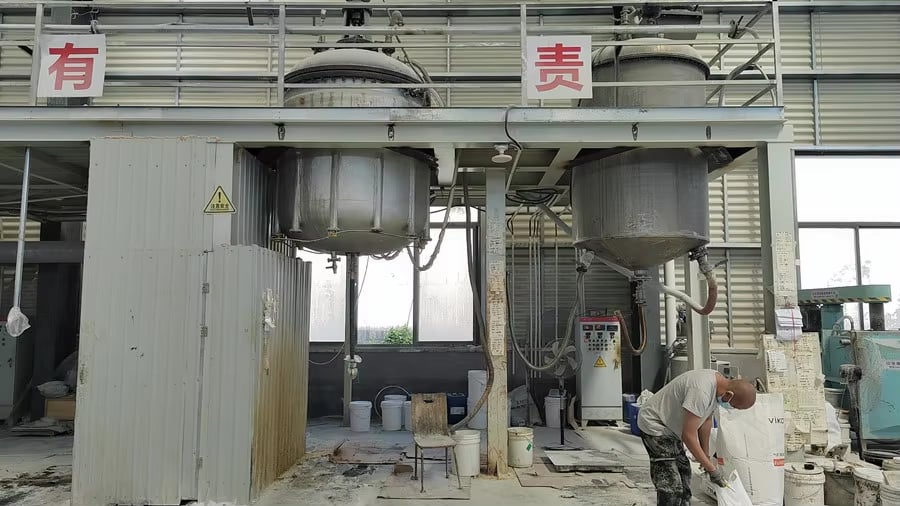 Reactor Kettles
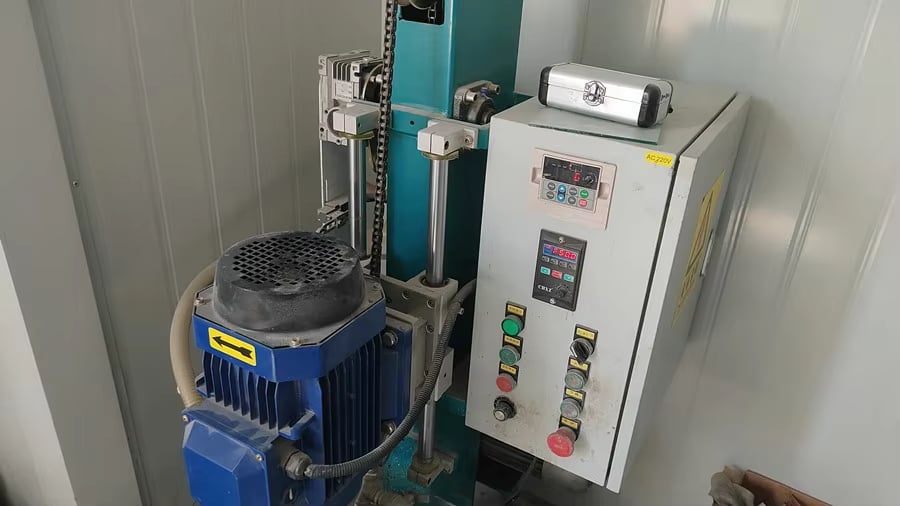 Dispersing Equipment
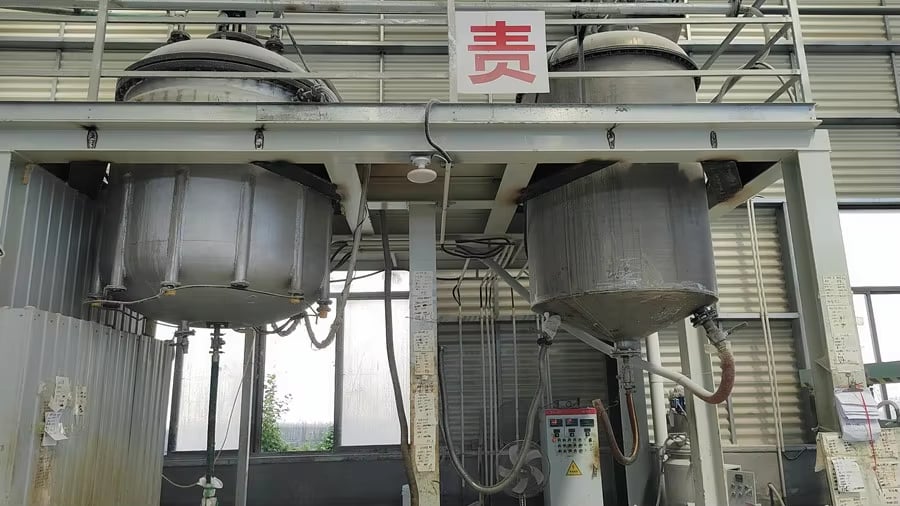 Mixing & Control
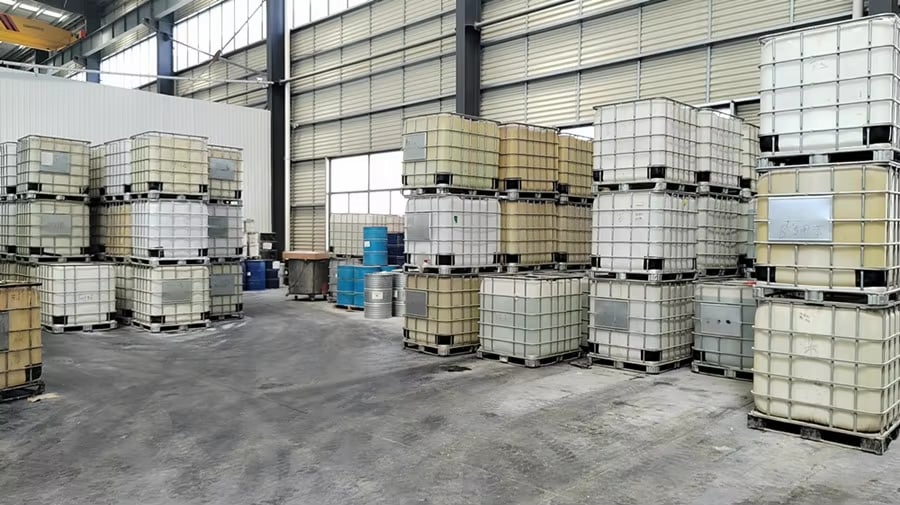 Raw-Material Store
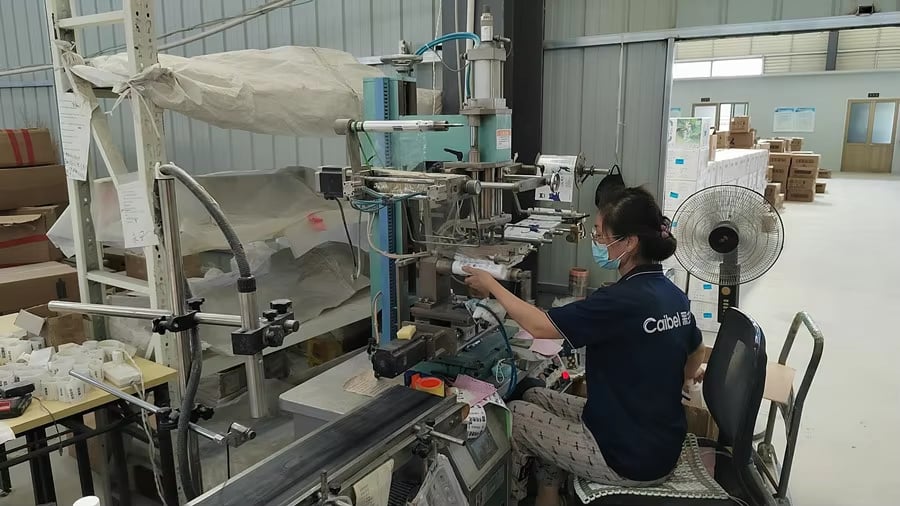 Labelling
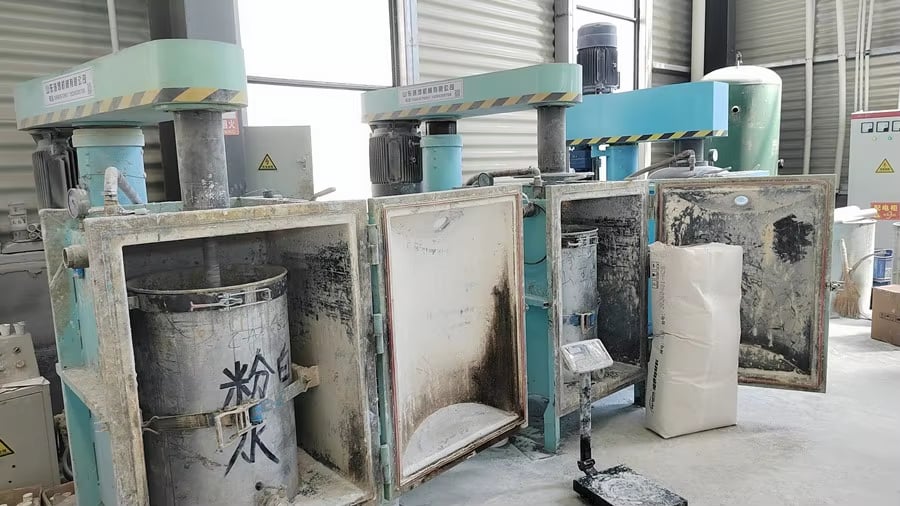 Vacuum Mixing
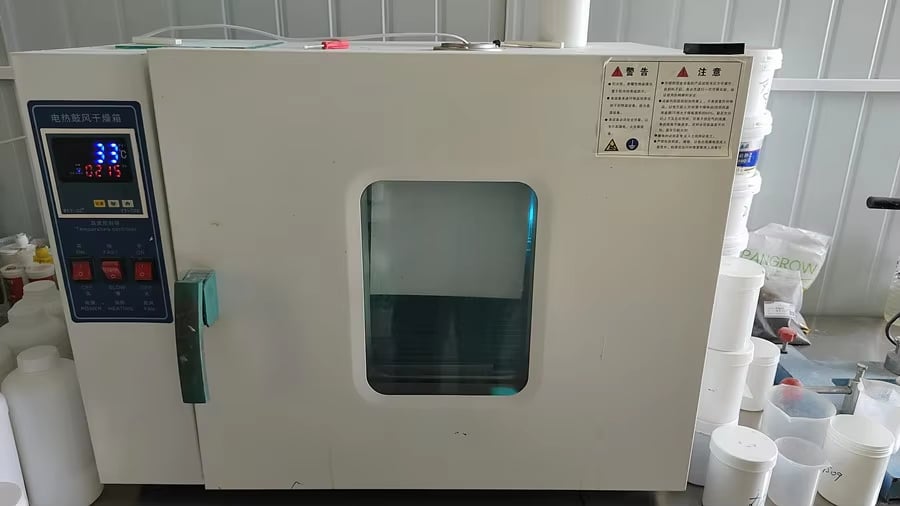 QC Drying Oven
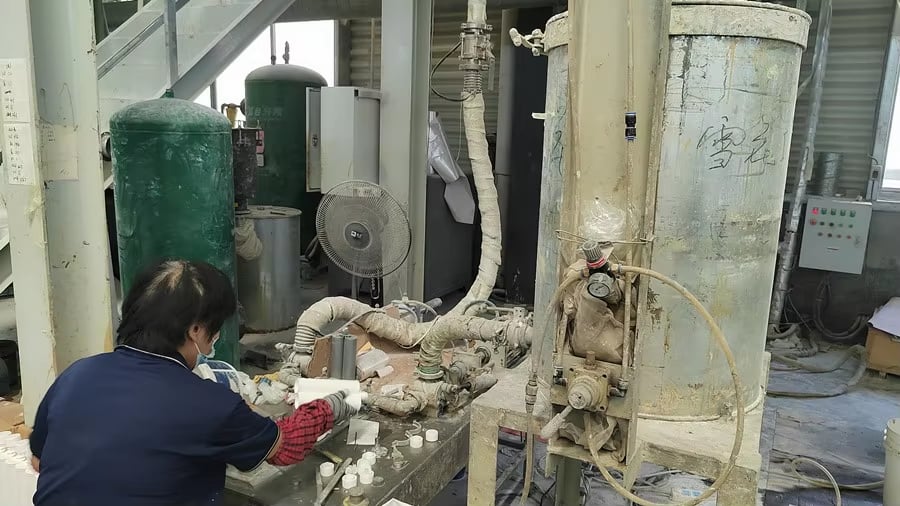 Filling & Capping
Questions about production, certificates or MOQ?
Ask Our TeamThis product line is verified by third-party laboratories. The marks shown above are the ones we publish as images; the documents behind them — certificate copies, batch-specific test reports, the CE Declaration of Conformity — are issued on request. A scanned badge proves nothing about your slab; the report behind it does.
Get a Free Quote
Send the floor area, substrate condition and what the room has to take. We reply with the system build-up, coverage estimate and an FOB quotation — usually within 24 hours.